
Time:2026-10-22
📌 Key Takeaways for Industrial Facility Managers & OEM Engineers:
Ingress Protection Integrity: Certified ip65 industrial smart lighting guarantees complete protection against dust ingress (Level 6) and resistance against low-pressure water jets from any angle (Level 5), eliminating internal component corrosion.
Intelligent Energy Optimization: Integrating an ip65 smart led fixture with Bluetooth Mesh or Zigbee wireless controls reduces facility energy consumption by 50% to 75% via dynamic daylight harvesting and occupancy sensing.
Illumination & Efficacy Standards: Modern heavy-duty luminaires deliver high ip65 lumens outputs exceeding 160 lm/W to 180 lm/W, maintaining target lux levels across high-bay manufacturing plants and damp processing halls.
Ruggedized Construction: Combining an ip65 light rating with IK08/IK10 impact resistance ensures uninterrupted operation across extreme thermal ranges (-40°C to +55°C) and high-vibration manufacturing environments.
Factory production lines, food processing plants, chemical facilities, and heavy-equipment manufacturing halls operate under harsh conditions. Fine airborne dust, metal shavings, humidity, and daily chemical washdowns subject electrical equipment to severe environmental stress. Traditional non-sealed indoor lighting fixtures rapidly deteriorate in these surroundings, leading to premature driver failure, optical degradation, and costly production downtime.
Deploying ruggedized ip65 industrial smart lighting solves these operational roadblocks. By pairing sealed IP65 ingress protection with automated controls, factory operators maintain safety compliance, reduce maintenance cycles, and cut facility energy overheads. This technical guide outlines engineering standards, optical metrics, control protocols, and quality assurance workflows for industrial lighting buyers.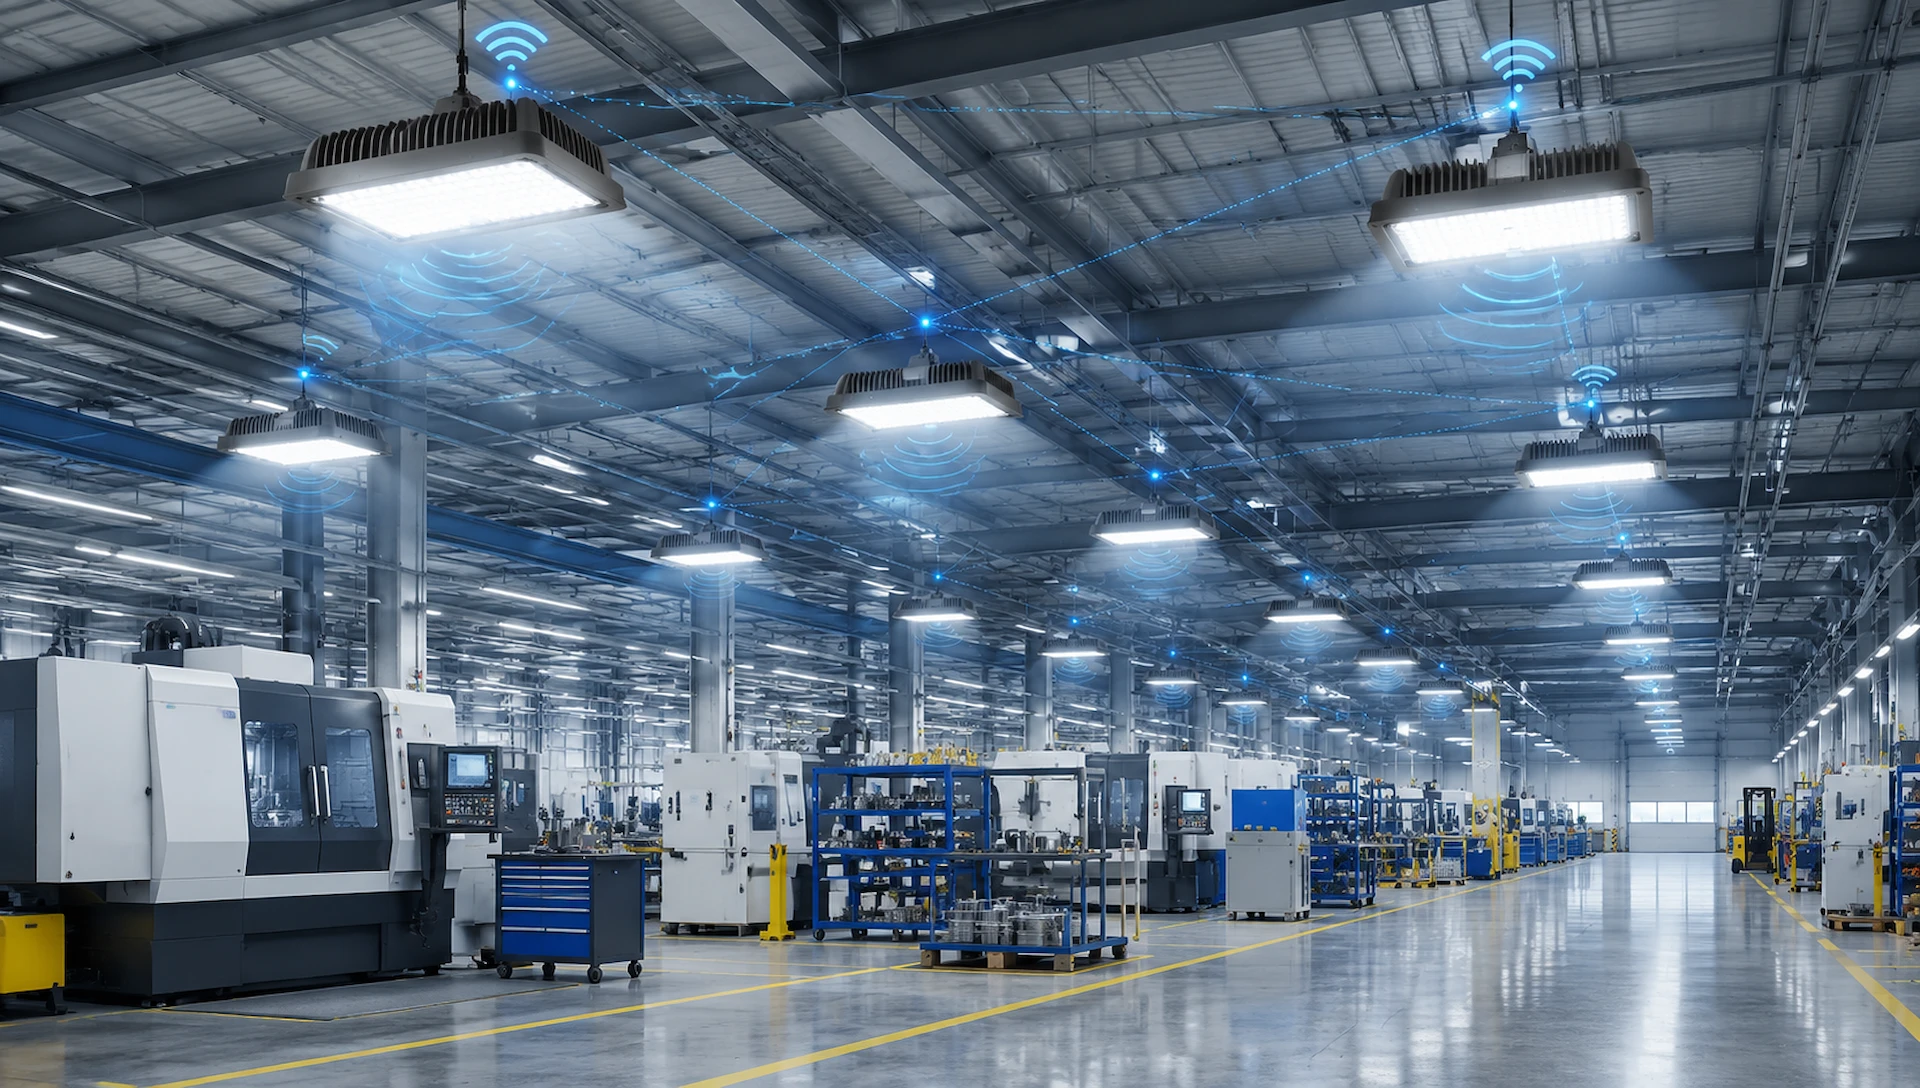
Selecting industrial luminaires requires a clear understanding of international ingress protection standards (IEC 60529).
An official ip65 led rating consists of two distinct numerical protection codes:
First Digit (6): Represents the highest level of dust ingress protection. Under vacuum test conditions, zero solid particles or conductive dust can penetrate the luminaire housing.
Second Digit (5): Confirms protection against water jets projected by a 6.3 mm nozzle from any angle at a pressure of 30 kPa and a flow rate of 12.5 liters per minute.
| Protection Rating | Dust Ingress Level | Water Protection Capability | Typical Industrial Environment |
| IP54 | Dust protected (limited ingress permitted) | Protection against water splashing | Dry indoor packaging lines, clean warehouses |
| IP65 | Dust-tight (zero particle ingress) | Protection against low-pressure water jets | Standard factory floors, processing plants, damp zones |
| IP66 | Dust-tight (zero particle ingress) | Protection against powerful high-pressure water jets | Exterior marine docks, severe chemical washdown zones |
| IP67/IP68 | Dust-tight (zero particle ingress) | Temporary or continuous water submersion | Submerged sumps, drainage pits, underwater tanks |
For a broader overview of factory-grade fixtures and environmental protection compliance, explore the 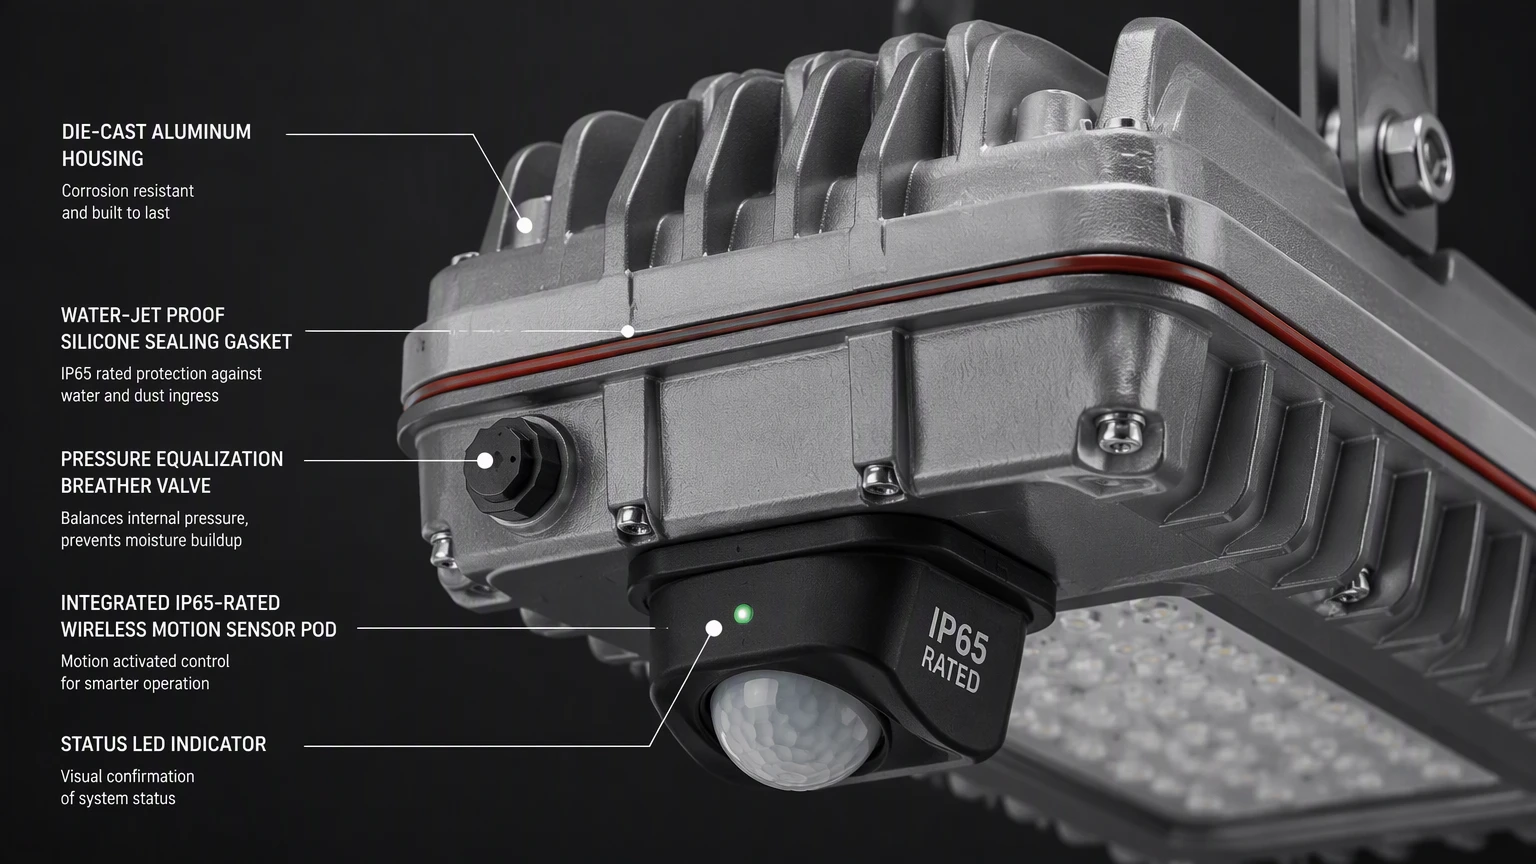
Industrial smart luminaires combine mechanical durability with embedded microcontrollers and multi-mode optical sensors:
Sealed Die-Cast Aluminum Housing (Thermodynamic Heat Sink)
High-Efficiency Optics Engine (160+ lm/W | 10,000 to 60,000 Lumens)
Silicone Gasket Seal & Pressure Equalization Breather Valve
Sealed Smart Control Pod (Integrated PIR/Microwave + Daylight Sensor)
Wireless Control Node (Bluetooth Mesh / Zigbee 2.4GHz RF Transceiver)
1. High-Output IP65 Lumens & Efficacy
Delivering adequate task-plane illumination across high-bay facilities (ceiling heights from 6 to 15 meters) demands powerful optical output. Commercial ip65 smart led high-bay fixtures deliver customizable ip65 lumens ranging from 10,000 lm to over 60,000 lm, maintaining high luminous efficacy (>160 lm/W). This ensures uniform lux levels without hot spots or worker glare.
Equipping an ip65 light rating luminaire with integrated motion and ambient light sensors eliminates energy waste:
Microwave Motion Radar: Detects movement through dust clouds and humidity, triggering light output instantly when forklifts or personnel enter an aisle.
Closed-Loop Daylight Harvesting: Automatically dims LED arrays when natural skylights illuminate the factory floor, preserving targeted illumination while minimizing kWh draw.
Maintaining an ip65 light rating across years of continuous industrial operation requires precise mechanical and thermal engineering.
Thermal cycling caused by turning high-wattage fixtures on and off creates internal pressure differentials. Without an internal breather valve, moist air is sucked past seals into the luminaire housing. Integrated waterproof PTFE membrane valves equalize internal pressure while blocking dust and liquid ingress.
Factory atmospheres frequently contain airborne oil mists and mild chemical vapors. Heavy-duty ip65 industrial smart lighting housings utilize electrostatically applied powder coatings that withstand 1,000+ hours of salt spray testing (ASTM B117), combined with IK08 to IK10 impact-resistant tempered glass or polycarbonate lenses.
To stay updated on changing industrial lighting regulations and product releases, read the latest articles in our
To verify structural integrity and electrical safety, manufacturing plants execute a 4-step quality assurance process for every ip65 industrial smart lighting fixture prior to shipment:
| QA Test Stage | Engineering Test Name | Verification Procedure & Acceptance Standard |
| Step 1 | Vacuum Dust Chamber Ingress Test | Fixtures undergo negative pressure vacuum testing inside a talcum powder chamber for 8 hours to confirm zero dust ingress. |
| Step 2 | Directional Water Jet Spray Test | High-volume water spray nozzles blast housing seams and cable glands from all angles at 12.5 L/min to check seal integrity. |
| Step 3 | Thermal Shock & Environmental Aging | Luminaires operate continuously at +50°C and -40°C inside climate chambers to verify driver stability and gasket elasticity. |
| Step 4 | Wireless Signal & Smart Sensor Calibration | Spectrum analyzers verify 2.4 GHz Bluetooth/Zigbee RF range and calibrate microwave sensor sensitivity limits inside optical test booths. |
Both ratings feature the highest "6" level of dust-tight protection. The difference lies in liquid resistance: IP65 protects against low-pressure water jets (12.5 L/min at 30 kPa), making it ideal for standard factories, damp warehouses, and general washdown areas. IP66 protects against powerful high-pressure water jets (100 L/min at 100 kPa), which is required for heavy chemical processing plants or exterior marine docks subjected to severe washdowns.
Yes. Premium industrial IP65 smart fixtures are engineered with heavy-duty die-cast aluminum heat sinks, thermal conductive gap pads, and industrial-grade LED drivers. This thermal management architecture allows luminaires to operate reliably in ambient temperatures ranging from -40°C in cold-storage warehouses up to +55°C near factory furnace lines.
Modern IP65 smart luminaires utilize external waterproof control pods or specialized radio-transparent polycarbonate windows. The Bluetooth Mesh or Zigbee wireless module resides behind an IP65-sealed UV-stabilized lens, allowing 2.4 GHz RF signals to propagate freely between fixtures without breaking the dust-tight and water-jet enclosure seal.
Implementing certified ip65 industrial smart lighting across your manufacturing plant lowers operational costs, meets strict international safety standards, and creates an optimized working environment for your workforce.
To request detailed product datasheets, evaluate sample fixtures, or discuss custom OEM integration with our engineering team,



+86 15899791249

+86 755 2955 3313


Address: Huafeng No.1 Science and Technology Park, Sanwei, Bao'an District, Shenzhen, Guangdong, China.
